
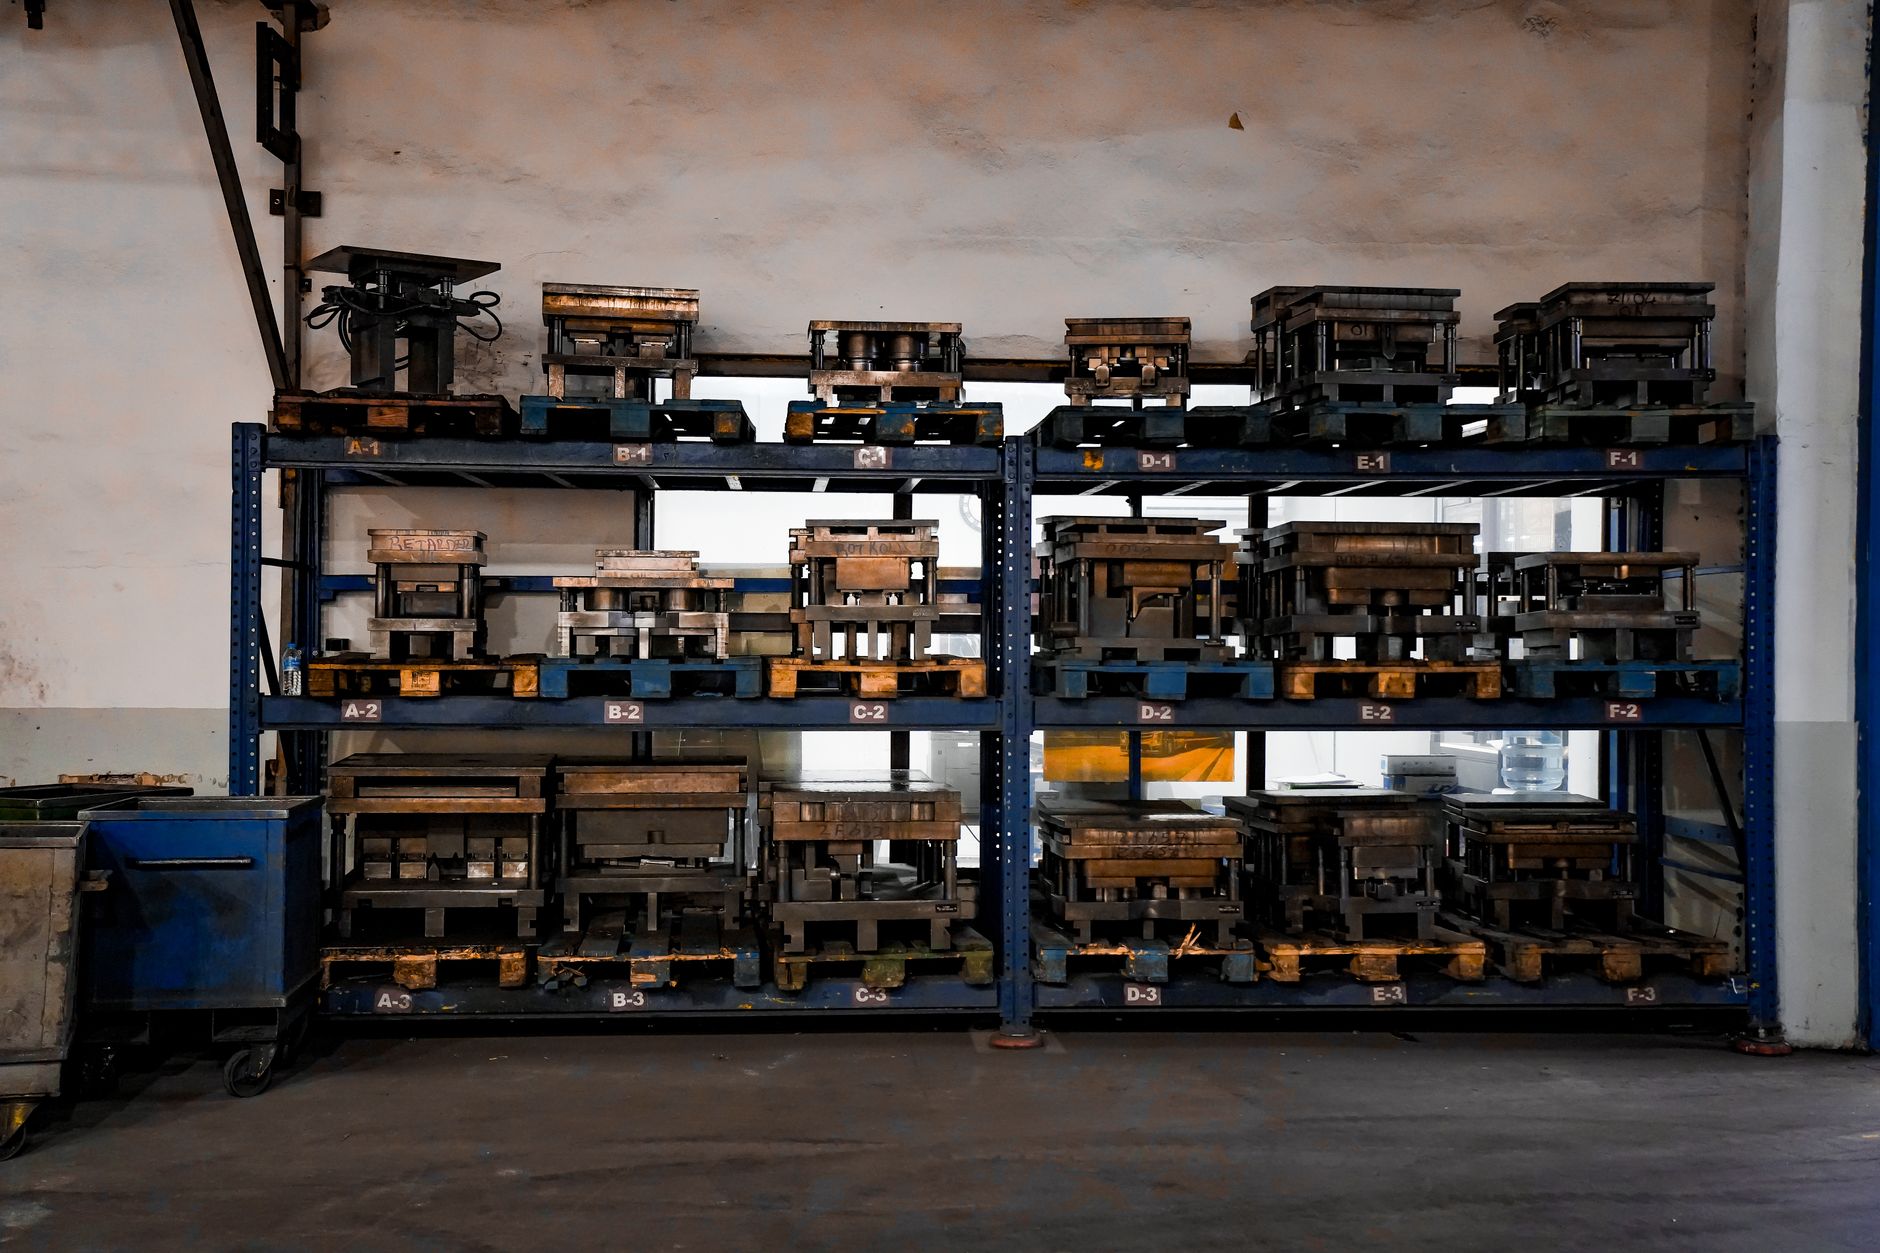
The question, in the buyer's words
I run a 160-person stamped metal parts plant where carts of bins move from presses to racks on all three shifts, and presses sit waiting on those moves; could autonomous mobile robots take those runs so we stop losing ground to rivals?
Key takeaways
- Mobile robots fit the repetitive bin runs between presses and racks, not die setting or press-side work.
- Presses wait for several reasons, and a robot only removes the wait caused by transport.
- Press guarding, lockout and pre-operation checks still apply to every cart and truck you add.
- Pilot one lane on one shift and measure idle press minutes before scaling up.
- A lease quote follows a free site assessment, so the price is set after your floor is measured.
Can mobile robots take stamping plant bin runs off the presses?
In most stamping plants the press is not the slow part. A press runs fast when it has blanks or coil and a clear exit, and the lost minutes usually come from the moves around it. When carts of bins sit at the press waiting for a tug or a driver, the press stops, and that lost output cannot be made up later on the same shift.
Mobile robots suit moves that repeat on a fixed pattern. A robot that carries a full bin cart from a press exit to a rack, then returns an empty cart to the press, follows a route, stops at known points and needs no judgment at each step. That is the kind of run a mobile robot can take on all three shifts without a person pushing the cart.
They do not suit every move. Loading dies, adjusting feeds, clearing jams and resetting a press after a die change stay with trained people. The realistic split is that robots take the transport share of the work and your people keep the press work.
Expect the first pilot to teach you more about your floor than about the robot. Routes, staging points and traffic will surface problems that a drawing does not show, which is why the first step should be a site walk rather than a commitment to a fleet.
Why do presses sit idle while bins wait?
A press waits for several reasons. It may lack blanks or coil, it may be between die changes, it may be held for a quality check, or it may be waiting for a full bin to leave the press exit. Only the last reason is a transport problem, and it is the one a mobile robot addresses.
Before you consider any robot, time the waits. Log each stop on each press for two or three full shifts and tag the cause. If transport is a small share of the stops, a robot will not change output much, and a simpler fix such as a second bin position or a staging rule may pay off sooner.
This is also where the worry about rivals needs care. A plant that loses ground usually loses it on press uptime and changeover speed, not on whether carts are pushed by hand. A tally of stop causes shows whether a robot touches your real gap.
- Repeat bin runs, press exit to rack
Autonomous Mobile Robot
Follows a fixed route at a steady pace on every shift, with no breaks and no drift in timing.
Staff
Can do it well, but gets pulled away for breaks, absences and other work, so pace varies by shift.
- Die change and press setup
Autonomous Mobile Robot
Does not take part, since the robot stays out of the die work and the press envelope.
Staff
Trained die setters handle it, with lockout and guarding rules applied at every step.
- Judgment at a jam or a bad blank
Autonomous Mobile Robot
Stops and calls for help but cannot tell why the press stopped.
Staff
Reads the press, the part and the sound, then decides what to do next.
- Night coverage when staffing thins
Autonomous Mobile Robot
Keeps running the planned route when the crew is short, inside its marked zones.
Staff
Has to be scheduled and covered, and each absence leaves the press waiting.
- Changing a route or adding a stop
Autonomous Mobile Robot
Needs a planned route change, a floor check and a test run before it goes live.
Staff
Adjusts on the spot with a supervisor's word, though the change still needs to be recorded.
What does the press workforce look like in the US?
The Bureau of Labor Statistics counted 179,230 people employed as cutting, punching and press machine setters, operators and tenders, metal and plastic, in May 2023. That is a large pool of experienced press people, and it is the same pool you compete with when you hire setters and operators.
The Bureau's Occupational Outlook Handbook projects employment of metal and plastic machine workers to decline 7 percent from 2024 to 2034. That projection covers the broader machine worker group rather than the press operator code alone, so read it as a direction for the trade, not a forecast for your region.
We did not find an official federal manufacturing quits rate for 2025 to set beside these figures. Pull turnover and open-shift counts for your own press and material handling roles, because those numbers decide how much a steady robot run is worth to your crew.
How many stamping plants are there, and how many use mobile robots?
An industry data aggregator, citing no year, lists 1,145 establishments and 46,966 employees under NAICS 332119, which covers metal crown, closure and other metal stamping except automotive. We have not verified that count against federal Census data, so treat it as a rough picture of the sector, not a precise total. Automotive stampers may be counted under a different code, so check your own classification.
Adoption figures for mobile robots are thinner than for arms. A3, the association for advancing automation, reported that North American companies ordered 36,766 industrial robots in 2025, up 6.6 percent in units from 2024, with cobots at 19.6 percent of those orders. A3's count covers industrial robot arms only, so it does not show how many stamping plants run mobile robots.
We could not find a verified share of stamping plants using autonomous mobile robots. Do not assume rivals have already automated their bin runs. Ask your own customers, suppliers and trade groups what they run before you treat a competitor's move as settled.
What safety rules apply to presses and the carts that move bins?
For mechanical power presses, the OSHA standard at 29 CFR 1910.217 requires a main power disconnect that can be locked in the off position, a substantial guard over foot treadles and a program of regular press inspections. Modifications must follow the standard's own requirements, so a robot lane that changes a guard or an access point needs engineering review before it runs.
According to OSHA's 1979 diesetting instruction, full-revolution mechanical presses generally cannot be guarded during die setting. A robot should never be routed into a press during setup, and die setting stays a controlled, locked-out task. Confirm which standards cover each press in your plant, since presses of other types can fall under different rules.
Powered trucks have their own record. OSHA's powered industrial trucks directive, an older archived document, says about 1.5 million US workers operate roughly 855,900 powered industrial trucks. A safety consultant's summary of OSHA data reported 78 work-related deaths and 7,290 nonfatal injuries with days away from work from forklift-related cases in 2020.
A 2024 trade analysis, cited by a safety center, linked about 15 percent of powered truck injuries, roughly 1,800 cases, to skipped pre-operation checks. Carts and robots do not remove that risk, they move it. Every unit needs pre-operation checks, a defined route, separation from pedestrians and an emergency stop your staff can run from day one.
How do robot lanes and the press line fit together on the floor?
Start by mapping the moves. Walk each press exit to each rack, count the carts per shift and note where they wait. Most stamping floors have a few repeat lanes, and those are where a mobile robot earns its place. A lane that crosses a forklift aisle, a rework cell or a dock door needs its own review before it goes on a schedule.
Staging points matter more than robot speed. Give each press a marked full-bin position and a marked empty-bin return, painted on the floor and enforced by the same rule on every shift. When the press exit and the robot pickup share a clear spot with clear rules, the robot waits less and the press waits less.
Plan the handoffs for people. An operator at the press still signals a full bin, and a material handler still clears a blocked lane. Those signals should be simple, visible and identical on every shift, so a new hire can run them on the first day.
Will robots cover all three shifts without a person on each run?
A mobile robot on the bin route can run on the third shift, when crews are thinnest and press idle time often grows. It needs no driver on each cart and takes no breaks, which makes its pace steadiest where your press crew is short.
Do not expect it to run unattended. Someone must watch exceptions, swap or charge units, clear a blocked lane and report faults. Name that role on each shift, even if it takes a fraction of one person's time, or a stopped robot will look like a failed robot.
Test the route in the hours you will run it. Lighting, press noise and traffic at night differ from the day schedule, and a route that works at noon can fail at two in the morning when the floor is quiet and dark. Plan those tests before the robot's first full shift.
How does leasing a mobile robot work with us?
We are an integrator, not a single-brand seller. We pick the robot that fits your floor across manufacturers, then lease it through financing, deploy and integrate it, train your staff and service it under our service plan with regional service engineers in every state we service. You work with one partner for the whole lifecycle instead of several vendors.
Our lease payment is quoted after a free site assessment. We measure your routes, staging points, press exits and traffic, then quote a lease for the units and lanes that fit the floor. A service plan included in the lease keeps repair and maintenance on one contract, with on-site dispatch and remote triage when a unit faults.
A sensible first step is one leased unit on one lane for one shift. That gives you measured press idle minutes before you commit to a wider fleet, and the quote shows what changes as you add units. Ask for the lease terms in writing, including response times for the third shift.
What should you check before you decide?
Start with the numbers you already have. Time the press stops for two or three full shifts, tag the cause of each stop and count how many bins wait longer than a set time. If transport is the largest cause, a mobile robot deserves a serious look. If it is not, work on changeover or material supply first.
Check the press controls and guarding on each press. Confirm that main disconnects can be locked off, that foot treadles are guarded and that the press inspection program is current, because a robot lane does not change those duties.
Ask who services the robots when a unit fails on the third shift, and what the response time is in writing. Ask whether a spare unit can cover a failed one. An idle robot lane leaves the presses waiting again, only in a different place.
Frequently asked questions
Upcoming manufacturing events
- Trade showBrats & RobotsNov 10, 2026Alliant Energy Center Exhibition Hall, Madison, WI
- Trade showMATE Farm & Ranch ShowFeb 11 to 13, 2027MetraPark, Billings, MT
- ExpoPFMA Expo 2027Feb 17 to 18, 2027Washington County Fair Park, West Bend, WI
- ExpoLouisville Facilities Maintenance ExpoApr 15, 2027Mellwood Art Center, Louisville, KY
Want a warehouse robot at your stamping press lines in manufacturing plants?
Tell us about your site. We will recommend the robot, quote the lease, and keep it serviced.
Sources
- Bureau of Labor Statistics, OEWS May 2023 profile for SOC 51-4031
- Bureau of Labor Statistics, Occupational Outlook Handbook, metal and plastic machine workers
- Industry data aggregator, NAICS 332119 establishment profile
- A3, North American robot orders in 2025
- OSHA 29 CFR 1910.217, mechanical power presses
- OSHA powered industrial trucks directive (archived)
- Safety consultant summary of OSHA forklift injury data
- Safety center summary of powered truck pre-operation check statistics