Key takeaways
- Short runs with frequent changeovers usually favor a movable cobot over a hard tooled cell.
- Changeover gains come from tooling and fixtures as much as from the robot itself.
- Footprint and payback figures in this market are mostly vendor reported, so measure your own aisles and job mix.
- No independently verified intervention rates exist for fixed press cells, so count your own operator stops for a month.
- Guarding requirements can change the floor math, so raise them in the risk assessment before sizing anything.
Which setup suits a short run?
For a shop that runs many small batches, a cobot tending a small press usually beats a fixed automation cell on the two costs that hurt most: changeover time and floor space. A fixed cell earns its keep when one part runs long enough to justify hard tooling and dedicated fixturing. When the job mix shifts every few days, an arm that can be moved, reprogrammed and parked is the easier fit.
The research we reviewed supports that direction but not precise numbers. Most figures below come from vendors, integrators or older trade articles, and we flag each one. We found no independently verified figures for fixed press cell changeover, footprint or operator stops, so part of this comparison rests on how the work is actually done.
How long does changeover take on each setup?
Changeover on a press brake is largely a tooling problem. A 2013 trade article quoting Scott Ottens of Amada America put tooling setup at about 6 percent of time on each bending job, and named tooling changeover as a bottleneck for small batches. That article is old and concerns press brakes, but the underlying problem has not gone away.
Newer equipment narrows the gap without any robot. The Fabricator reports that Accufab, a small shop in Georgia, runs two newer press brake systems that cut changeover between bending jobs to under 15 minutes. Those are fast changeover brakes rather than cobots, and the article did not state a date in the result we reviewed.
A vendor comparison describes hard tooled lines with changeover measured in hours, against minutes for cobot changeover. That figure is vendor reported, and we could not verify it independently.
How much floor space does each cell need?
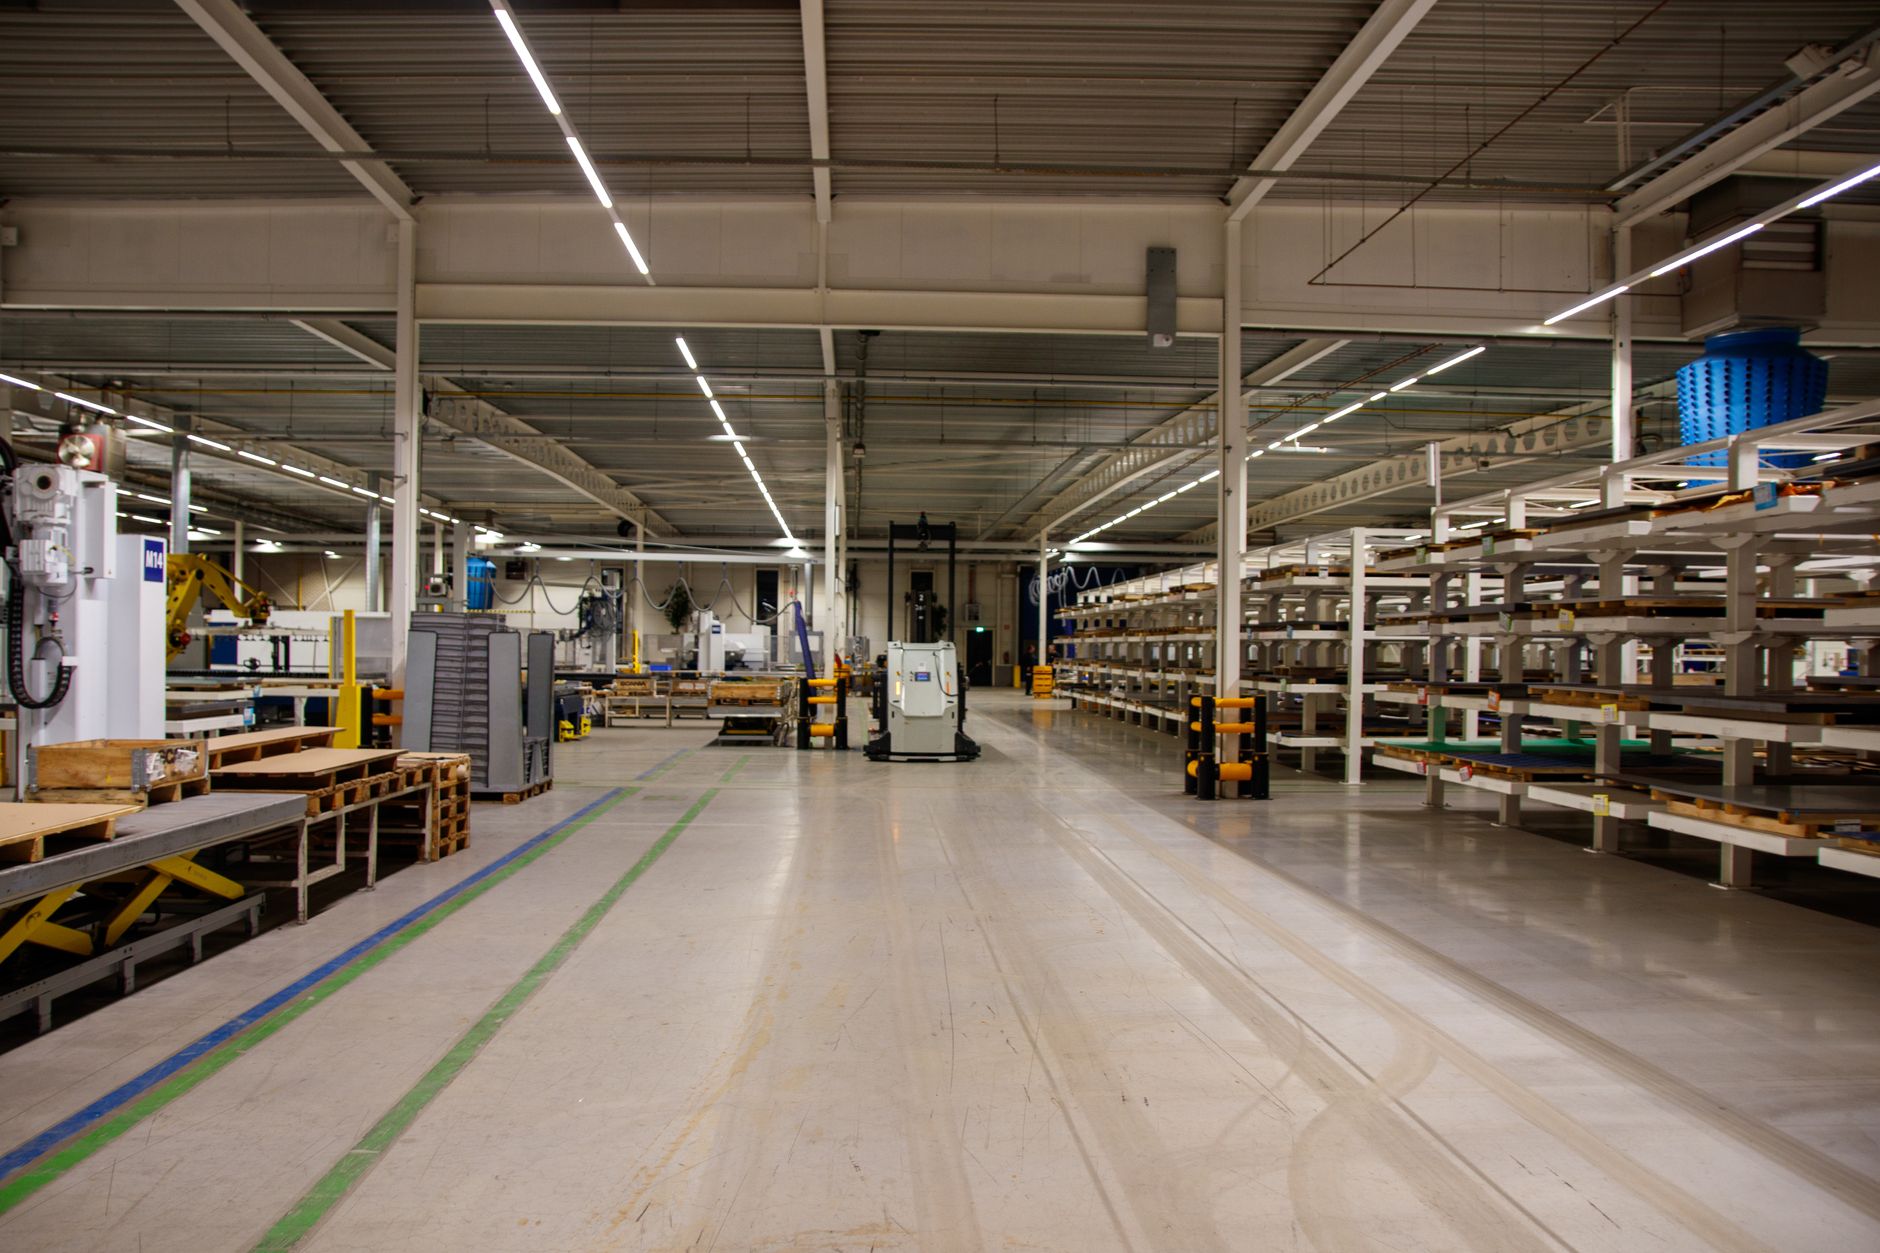
Footprint is where the two setups diverge most in plain geometry. One integrator compares a 10 kg industrial arm that needs a 3 by 4 meter fenced zone with a cobot that shares a 1.5 by 1.5 meter worktable with an operator. Those figures are vendor reported, so use them as a starting point and measure your own aisle.
Mounting also matters. Olympus Technologies, a UK integrator, reports that its press brake tending cobot can sit on a fixed or mobile stand, so the brake can still run manually for low volume parts. A rotating cylinder reorients the parts, and the source gave no changeover figures. A cell bolted to the floor is fixed infrastructure. A cobot on a movable base can be wheeled to another station within a shift, though that depends on the base and the cell design.
How often will an operator have to step in?
We could not find a verified intervention rate for fixed press cells, so we cannot offer a sourced comparison of stop counts. What we can describe is where the stops come from on either setup: part presentation, misfeeds, blanks that arrive out of spec and tooling that drifts out of position. A reorienting fixture removes a manual flip, but a cobot cell still needs a person to refill blanks, clear jams and check parts.
The honest test is a month of your own logs. Count every operator touch by reason, then compare that against what a fixed cell would need for the same parts. Your number will say more than any brochure.
Do batch size and cycle time settle the choice?
One vendor tending guide gives thresholds of more than 200 pieces per setup and machine cycle times over 90 seconds as the zone where cobot tending makes sense. That is one vendor's opinion, not an industry standard, and it fits poorly with a shop whose typical run is a few dozen parts.
Cycle speed still matters. Cobots are generally slower and lighter duty than industrial arms, so a press that cycles very fast may outrun the arm, and a fixed cell may be the better tool for that one part. Batch size and cycle time should be read together, not separately.
What do the payback numbers really show?
Standardbots, a cobot maker, puts cobot payback at 8 to 18 months depending on application, utilization and labor displaced, and cites 7 to 14 months across its small business deployments. Those are vendor figures, and they assume the cell runs steady work.
The payback clock starts only when the cell runs the work it was chosen for. For a small shop, utilization across several small jobs is the number to model, not the best case for one part.
What guarding does to the floor math
One source argues that cobots can often run without full fencing after a risk assessment, but an arm carrying a blade, a hot part or a heavy tool usually needs guarding or presence sensing. That requirement changes the footprint comparison above, because the guarding takes floor space too.
Ask your integrator to carry the guarding into the site sizing from the first visit, not after the cell is drawn.
A checklist for your job mix
Work through these measures before you request any quote. Each one turns a vendor claim into a figure from your own floor.
- Count distinct part families you run in a typical month, not total parts shipped.
- Time three recent press setups from last good part to first good part, with a stopwatch.
- Note the batch size where tooling cost per part starts to outweigh the cell's cycle time.
- Log every operator touch per shift by reason, such as blanks, jams and part checks.
- Measure the clear floor path and aisle width where an arm or mobile base would travel.
- Get the guarding requirement from the risk assessment before you size the cell.
Where a lease quote fits the decision
Service Robot Co. is an OEM neutral integrator, so we pick the cell that fits the job mix rather than one manufacturer's catalog. We lease robots on a three year lease, with one fixed payment quoted after a site assessment.
Integration, operator training and RoboCare service come with the same engagement, so a shop with a changing job mix has one contact for the arm, the guarding and the service calls. Bring your changeover times and operator logs to the assessment, and the quote will rest on your numbers.
Frequently asked questions
Want a robot working for you?
Tell us the job and the site. We will recommend the robot, quote the lease, and keep it serviced.
Sources
- The Fabricator: The Time Between Runs (Accufab changeover)
- The Fabricator: Tooling Changeover Can Be a Pressing Issue (2013)
- Automate UK: Cobot Is Best Option for Engineering Firm Needing Press Brake Machine Tending Role
- EVS Integration: Cobot footprint and cell layout
- LANPDT Tech Talk Episode 18: Cobot safety and guarding
- Automation Inside: High-Mix Low-Volume Machine Tending with Cobots
- Racklify: Cobots (Collaborative Robots) in Industrial Applications, Integration and ROI
- Standardbots: Robots for Manufacturers, A Guide