Key takeaways
- Bead inspection cobots earn hours when the same joint geometry repeats but human vision fatigue sets in after an hour.
- Repair is a separate program from inspection: the arm should not auto-dispense without a verified defect list.
- Lighting and contrast matter more than camera resolution on glossy beads and dark substrates.
- Traceability logs should tie each pass to a serial or batch ID your quality system already uses.
- A vendor neutral integrator can pilot one station before you expand cobot rental across a second shift.
Where do cobots actually help on adhesive bead inspection?
Dispensed sealants and structural adhesives fail in quiet ways. A bead can look closed while missing coverage at an inside corner, or smear wide enough to foul assembly at the next station. Manual inspection works until volume and repetition blur the same defect across hundreds of panels per shift.
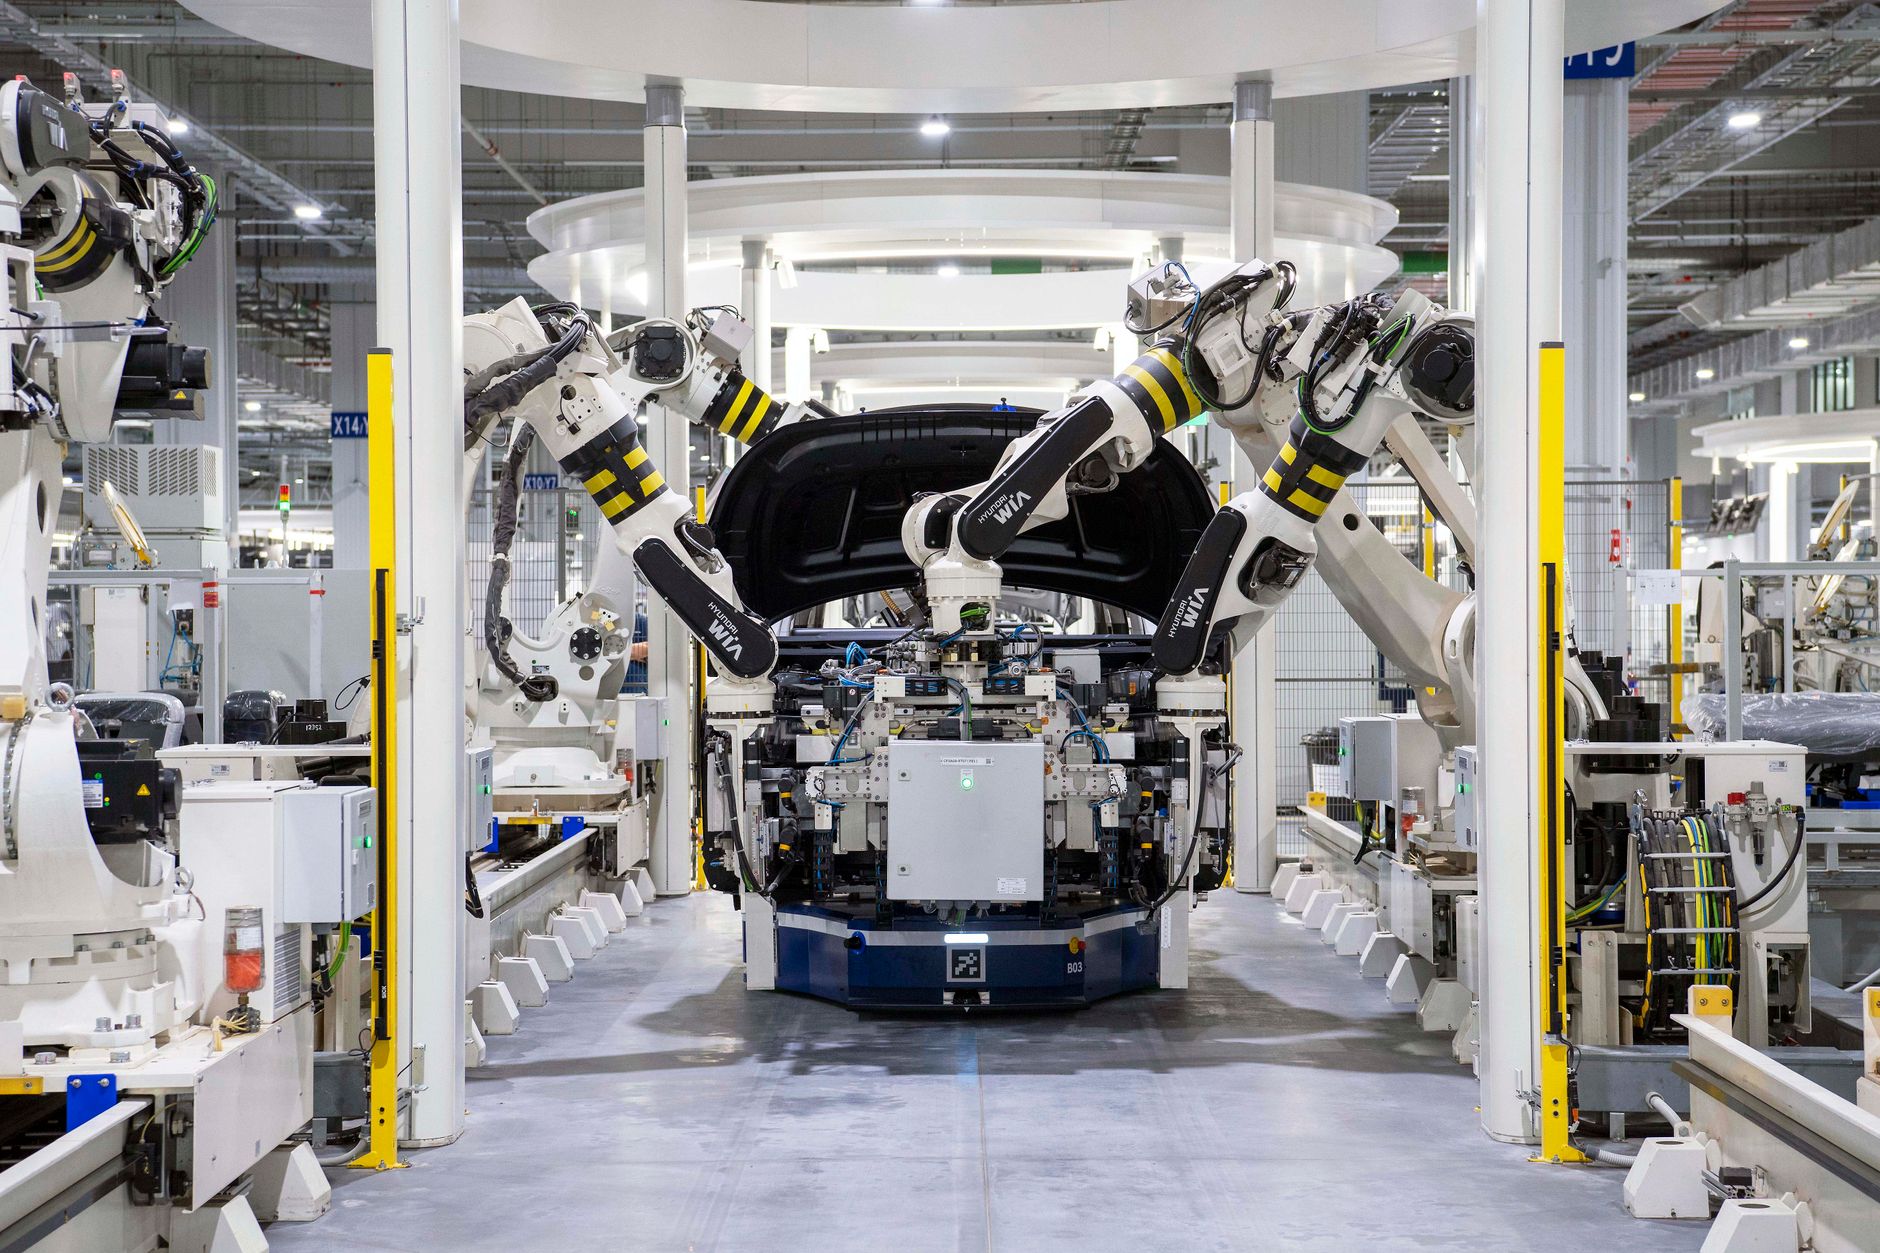
Collaborative robot arms with vision fit when the joint path is repeatable and the camera can see the bead without fighting glare. The cobot moves a sensor along a taught path, compares width and continuity to limits, and flags gaps for repair or reject. It does not replace your material approval process or the engineer who sets those limits.
Cobots are a poor default on one-off prototypes or beads hidden inside closed sections. They shine on windshields, appliance housings, battery trays, and other lines where the same bead profile runs all day and rework cost is high.
Why is bead continuity harder to judge than it sounds?
Operators catch obvious skips quickly. They miss short breaks at flange transitions, thin spots after nozzle wear, and squeeze-out that reads fine at arm length but fails leak test later. Shift change makes inconsistency worse because each inspector calibrates eyes differently.
According to the U.S. Bureau of Labor Statistics, manufacturing reported 355,800 total recordable injury and illness cases in 2023, with 224,400 cases involving days away, restriction, or transfer. Inspection and rework stations contribute through repetitive motion and awkward reaches even when the root cause is not the bead itself.
Robot inspection works when limits come from process engineering, not from the camera guessing. Width, position, and break length thresholds should be documented before anyone teaches a path on production parts.
How should vision setup handle gloss, color, and joint geometry?
Dark beads on dark metal need structured light or angled illumination more than a higher megapixel sensor. Clear adhesives on glass may need UV trace or background contrast aids approved by your material supplier.
Fixtures should present the same joint angle every cycle. A five degree tilt change can look like a width defect to naive edge detection. Teach on oily, dusty, and slightly misaligned samples from the floor, not only on golden panels.
High-mix lines can swap programs by SKU bar code instead of re-teaching every morning. Keep camera calibration on a schedule tied to nozzle change events, not calendar dates alone.
When does automated repair make sense versus human touch-up?
Repair means re-dispense, manual wipe, or localized re-run under a defined defect code. A cobot can present the joint to a handheld gun or carry a small applicator on the wrist when volumes justify tooling cost.
Auto repair without a confirmed defect is how you hide process drift. The workflow should require an inspection fail, supervisor acknowledgment for certain codes, and a second scan after touch-up before release.
Some materials cure too fast for robotic repair unless the cell sits close to the dispense station. Distance and open time belong in the same feasibility review as reach and cycle time.
- Separate inspection PASS and FAIL paths in the PLC map.
- Log defect type, location along the path, and repair operator ID.
- Block shipment if second-pass inspection still fails limits.
What traceability should the cell record?
Each cycle should store serial or lot, program ID, camera exposure settings version, and pass fail result. When a field issue returns, you need to know which limits were in force that day.
Link results to dispense parameters when possible: pressure, speed, and temperature at the upstream pump. Bead defects often trace to nozzle wear before they trace to inspection tuning.
Export data in the format your MES or quality team already consumes. A beautiful robot log that nobody reads adds no audit value.
How do you validate a pilot without fooling yourself?
Run side by side with human audit on the same panels for at least one full production week. Measure false accept and false reject rates separately. A robot that catches everything but stops the line on cosmetic variance will not survive.
Include known bad samples in the daily startup check. If the cell cannot reject a deliberate gap on the first shift, do not trust it on the tenth.
Cobot rental for manufacturing with monthly service included lets you keep the pilot on operating budget while engineering fixes upstream dispense variation.
When does outside integration beat adding another inspector?
Plants often hire a second quality tech before they fix lighting or fixture repeatability. Service Robot Co. acts as a full service commercial robot integrator for U.S. factories. We are OEM neutral on arms, cameras, and lighting, then finance, deploy, integrate, train, and service through a nationwide engineer network.
A first site visit maps joint types, cure times, and where repair must stay manual. One bead family on one line is enough to prove traceability and false-alarm rates before you tie the cell to customer release paperwork.